Table of contents:
Factors to Consider: Speed, Accuracy, and Material Durability
Comparing Checkweigher Models for Aquatic Product Lines
Understanding Dynamic Zero Tracking and Anti-Vibration Algorithms
Choosing Between Modular and Integrated Conveyor Systems
Factors to Consider: Speed, Accuracy, and Material Durability
The performance of a checkweigher largely depends on its speed, accuracy, and durability. A high-speed checkweigher ensures food products are weighed quickly without compromising accuracy, which is essential for meeting production quotas. Look for systems with advanced sampling technologies, such as the high-speed sampling systems offered by top checkweigher manufacturer like Macinte. Accuracy is equally crucial, especially for products with strict weight specifications like seafood or individually packaged items. Models with dynamic zero automatic tracking and anti-vibration algorithms ensure precision even in fast-paced environments. Furthermore, the durability of materials, such as 304 stainless steel, is vital in food processing to ensure hygiene, corrosion resistance, and long-term cost efficiency.
Comparing Checkweigher Models for Aquatic Product Lines
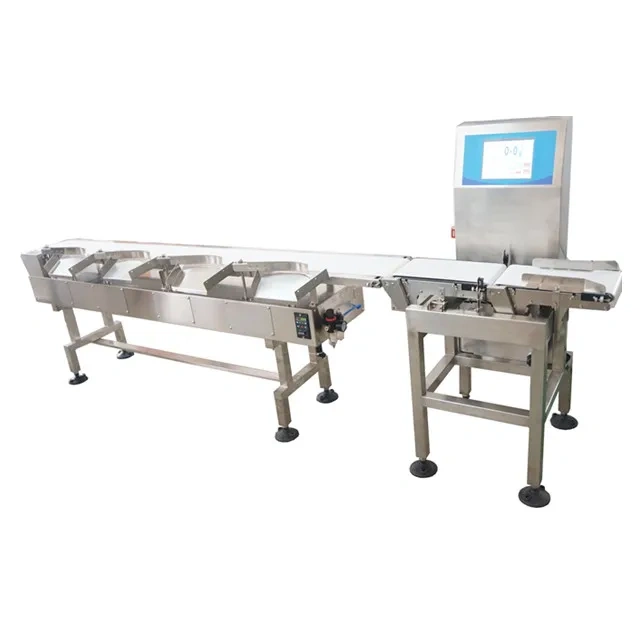
For food industries focused on aquatic products like shrimp, fish, and lobster, the requirements for checkweighers are unique. Manufacturers like Macinte offer specialized sorting machines equipped with dynamic weighing technology and filters specifically designed for seafood classifications. These systems cater to specific needs like real-time weighing, precision sorting, and efficient automation, all while reducing labor costs. Features such as modular assembly structures make maintenance and cleaning convenient, which is critical in preventing contamination in seafood processing facilities. Opt for a model that can distinguish between small weight variations, as some seafood tasks may require precision down to ±1g.
Understanding Dynamic Zero Tracking and Anti-Vibration Algorithms
Dynamic zero tracking and anti-vibration algorithms are game-changing technologies in checkweighing systems. The dynamic zero tracking functionality allows the device to continuously maintain accurate weighing readings by automatically adjusting for minor shifts in the weighing conveyor’s zero-point value. This ensures your products are consistently weighed even during prolonged operations. Anti-vibration algorithms, such as the FIVDSP technology, mitigate environmental interferences caused by vibrations or sudden movement in the system, making them ideal for active production lines that handle sensitive food items. These innovations directly contribute to better accuracy and reliability, reducing the risk of incorrect weight rejection.
Choosing Between Modular and Integrated Conveyor Systems
Another critical decision to make is whether to select a modular or integrated conveyor system for your checkweigher. Modular conveyor systems are highly flexible, allowing different components to be assembled or replaced separately, which is particularly useful for businesses with evolving production requirements. They also simplify cleaning, a critical advantage in food safety compliance. Conversely, integrated conveyor systems offer streamlined designs that minimize setup complexities and maximize throughput by reducing transition points. This can be especially beneficial in high-speed production environments. Evaluate your business’s workflow and maintenance priorities to determine the most suitable option.
To ensure success, partner with a trusted checkweigher supplier specializing in advanced technologies tailored to your specific needs. For example, Macinte, backed by 19 years of industry experience, offers cutting-edge dynamic checkweigher systems designed for various applications, including seafood and other food products. Their expertise in dynamic zero tracking, FIVDSP algorithms, and high-precision modular designs makes them a standout choice for businesses aiming to optimize efficiency and reliability in their operations.
Comments
Post a Comment