Table of contents:
A Comprehensive Guide to 6000 LPH Reverse Osmosis Systems
Understanding the Cost-Benefit Analysis of Industrial RO Equipment
How to Integrate High-Capacity RO Plants into Existing Water Treatment Systems
Future Trends in Reverse Osmosis Technology for Water Purification
A Comprehensive Guide to 6000 LPH Reverse Osmosis Systems
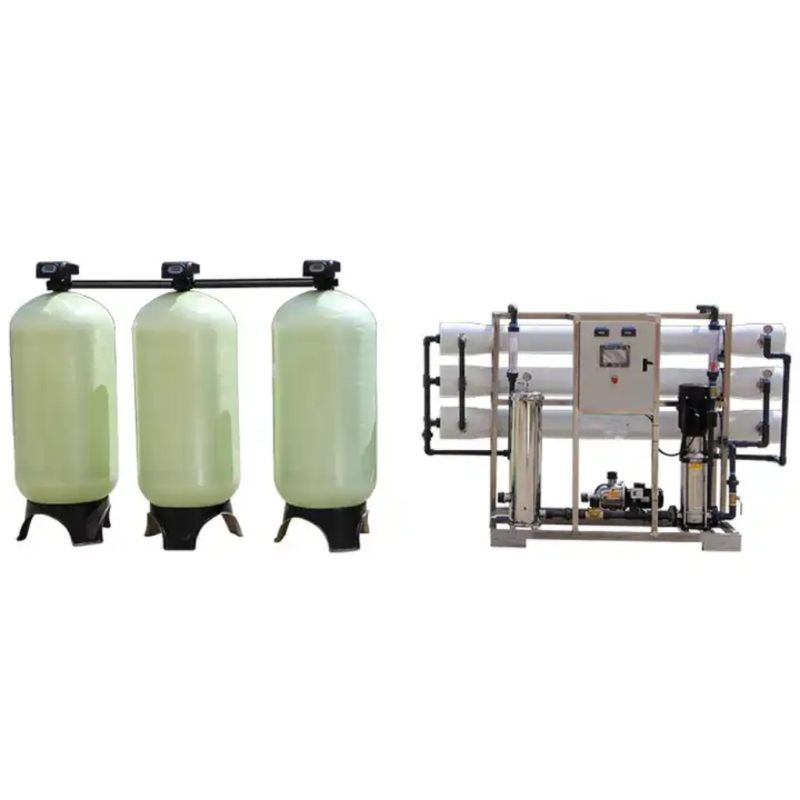
The 6000 LPH RO system represents a pinnacle in water purification plant technology. These high-capacity units, designed by expert reverse osmosis equipment manufacturers, offer a robust solution for businesses with substantial water treatment requirements. The system's core components include a water tank for raw water storage, a booster pump, quartz sand and carbon filters, a water softener, and a security filter. The heart of the system lies in its high-pressure pump and RO membrane system, which work in tandem to remove dissolved salts, colloids, microorganisms, and organic matter with an impressive 99% removal rate. This level of purification ensures that businesses can rely on a consistent supply of high-quality water for their operations.
Understanding the Cost-Benefit Analysis of Industrial RO Equipment
When considering the implementation of a water purification plant, business owners must carefully weigh the costs against the long-term benefits. While the initial investment in a 6000 LPH RO system may seem substantial, the advantages often outweigh the expenses. Reverse osmosis equipment manufacturers have engineered these systems to be energy-efficient and low-maintenance, reducing operational costs over time. The compact stainless steel design of modern RO plants also minimizes space requirements, making them suitable for various industrial settings. Moreover, the high water production capacity and ability to remove bacteria and heavy metals translate to improved product quality and compliance with stringent water standards, potentially opening new market opportunities for businesses.
How to Integrate High-Capacity RO Plants into Existing Water Treatment Systems
Integrating a 6000 LPH RO system into an existing water treatment infrastructure requires careful planning and expertise. Water purification plant specialists recommend a phased approach to ensure seamless integration. The process typically begins with a comprehensive assessment of current water quality and treatment processes. Reverse osmosis equipment manufacturers often provide customization options to tailor the system to specific business needs. Key considerations include the installation of pre-treatment systems, such as water softeners and carbon filters, to protect the RO membranes and extend their lifespan. Additionally, businesses should plan for the implementation of control systems that offer both manual and automatic operation modes, ensuring flexibility and ease of use.
Future Trends in Reverse Osmosis Technology for Water Purification
The future of water purification plant technology is promising, with ongoing innovations driven by leading reverse osmosis equipment manufacturers. Emerging trends include the development of more efficient membranes that require less energy and produce higher yields. Smart monitoring systems are becoming increasingly prevalent, allowing for real-time performance tracking and predictive maintenance. Additionally, there is a growing focus on sustainability, with manufacturers exploring ways to reduce waste and improve water recovery rates. As businesses continue to prioritize water conservation and quality, the demand for advanced RO systems is expected to rise, prompting further advancements in the field.
The landscape of industrial water purification is evolving rapidly, with 6000 LPH RO systems at the forefront of this transformation. These high-capacity plants offer businesses a powerful tool for ensuring water quality and operational efficiency. As reverse osmosis equipment manufacturers continue to innovate, the technology becomes more accessible and adaptable to diverse industry needs. By embracing these advanced water purification solutions, businesses can not only meet their current water treatment requirements but also position themselves for future growth and sustainability in an increasingly water-conscious world.
Comments
Post a Comment